PPE field note
PPE Procurement: Who Pays, What It Costs, and the Checklist That Keeps You Compliant
Posted on 2026-08-31 by Maeve Callahan
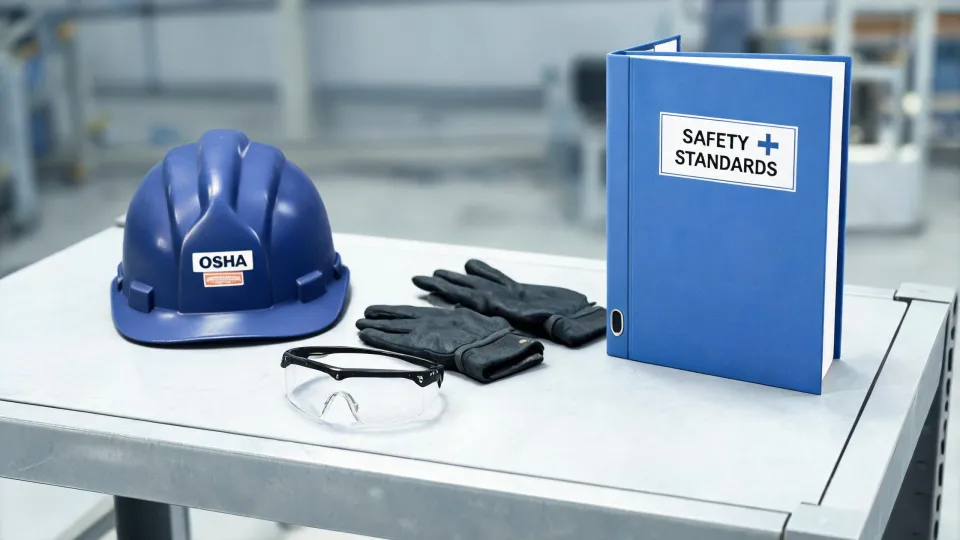
-
Step 1: Confirm Legal Responsibility for PPE Payment
-
Step 2: Calculate True Cost of Ownership, Not Just Unit Price
-
Step 3: Match PPE to Your Actual Hazards, Not the Catalog
-
Step 4: Get Quotes From Multiple Sources—Including At Least One Manufacturer
-
Step 5: Build a Compliance and Reorder Review Loop
- Common Mistakes I've Made (So You Can Avoid Them)
-
Final Notes
If you're a procurement manager, plant supervisor, or safety officer, you've probably asked the same question I hear constantly: who is responsible for paying for PPE? The short answer: employers. The longer answer involves a handful of OSHA rules, a few gray areas, and a purchasing process that costs more than it should if you only look at unit price.
This checklist is for anyone who buys PPE for a team of 20 or 500 and needs a practical, repeatable process. I've organized it into five steps, plus the mistakes I've made so you don't have to repeat them.
Step 1: Confirm Legal Responsibility for PPE Payment
OSHA's PPE payment requirements are clear: employers must pay for most PPE. That includes hard hats, gloves, safety glasses, rubber boots, respirators, and hearing protection. According to OSHA's PPE payment standard (29 CFR 1910.132(h)), the employer covers the cost of PPE except in limited cases like ordinary prescription safety eyewear or specific items employees choose to keep after leaving.
I remember auditing our 2023 spending and discovering we'd been reimbursing employees for rubber boots individually, then also buying them through our safety supply vendor. That's a double-pay situation. Once we centralized PPE purchasing under one approval code, we cut about 14% off our safety budget in Q3 alone.
One gray area: if PPE is employee-owned and the employer allows it, the employer doesn't have to pay for it. But if compliance requires specific standards (like ANSI Z87.1 for eyewear), you're responsible for ensuring the equipment meets that standard. If it doesn't, pay for it yourself. In my experience, just paying for it directly is almost always simpler.
Step 2: Calculate True Cost of Ownership, Not Just Unit Price
The $11 glove vs. the $14 glove—which is cheaper? I've seen procurement teams choose the lower quote every time, then watch the cheaper gloves fail in two weeks. The $14 gloves last six weeks. That's $11 vs. $4.67 per week of use. The "more expensive" glove is actually the deal.
I built a simple cost calculator after getting burned on hidden fees twice. Here's what I include:
- Unit price
- Shipping and handling
- Expected lifespan in your specific environment
- Change-out labor time
- Inventory carrying cost
- Compliance risk if the product fails
For example, when comparing cut-resistant gloves for our metal fabrication line, I calculated a total cost difference of about 38% between the cheapest initial quote and the option we ultimately chose. The cheap pair needed replacing 4x more often, and every replacement required a worker to walk 200 feet to the tool crib.
This is where working with an in-house manufacturer like Magid Glove and Safety Mfg Co can simplify things. Because they produce the goods themselves, there are fewer middlemen inflating costs and more consistency in quality. That doesn't mean they're always the cheapest—but they've been competitive every time I've run their quotes through my TCO model.
Step 3: Match PPE to Your Actual Hazards, Not the Catalog
PPE is not one-size-fits-all. I know that sounds obvious, but I've walked into plants where every worker wore the same glove regardless of job function. Then someone gets a laceration because the task required a higher cut level.
Use your hazard assessment (required by OSHA) as your shopping list. For example:
- Workers handling sheet metal need ANSI A4 or A5 cut-resistant gloves.
- Anyone near electrical panels needs arc-rated clothing, not flame-resistant cotton.
- People working near baluster railing installation or framing often need hand protection with grip, not just impact protection.
I want to say we do this perfectly now, but don't quote me on that—we still have to correct course occasionally. In 2024, we switched our baluster railing crew from standard work gloves to a high-grip, cut-resistant style. The unit cost went up $1.50 per pair. Hand injuries went from 3 recordables in 2023 to zero in 2024. That's a $14,899 workers' comp claim avoided (state average per hand injury, not ours).
Step 4: Get Quotes From Multiple Sources—Including At Least One Manufacturer
There are two ways to buy PPE: through a distributor or directly from a manufacturer. Distributors offer convenience and consolidated billing. Manufacturers often offer better pricing on volume, plus direct technical support.
I get quotes from at least three sources for every major PPE category. One of those needs to be a manufacturer. For gloves specifically, magid-glove is always on my list because they run their own manufacturing facilities. The "magid glove and safety mfg" search usually surfaces their corporate site, but I've found it faster to call their sales team directly.
Here's a real comparison from Q2 2024 when we reordered chemical-resistant gloves:
- Distributor A quote: $4.20/pair, no volume discount, 2-week lead time.
- Distributor B quote: $3.85/pair, volume discount 5% at 500 pairs, 3-week lead time.
- Magid Glove quote: $3.60/pair at 500 pairs, 1-week lead time.
Distributor B looked cheaper until I flagged that their 3-week lead time would've forced us to extend our previous order. That extension cost a $250 expedite fee plus overtime to cover the gap. Total TCO for Distributor B: $3.85 x 500 x 0.95 + $250 = $2,078.75. Magid total: $3.60 x 500 = $1,800. That's 13% difference hidden in lead time.
Step 5: Build a Compliance and Reorder Review Loop
PPE purchases aren't done when the products arrive. You need a review rhythm. I use a quarterly cycle:
- Audit PPE usage against the original hazard assessment.
- Track early failures or premature wear patterns.
- Check for updated standards (ANSI, NFPA, ASTM) that affect what you're buying.
- Renegotiate with at least one vendor—even just to confirm pricing hasn't changed.
When we audited in 2023, we found that 30% of our boot replacements were happening before 6 months of use, but our standard work boot contract was based on a 12-month life. We switched to a reinforced rubber boot with a different sole compound, and the average lifespan jumped to 11.7 months. The price was $8 more per pair. The replacement cost difference saved us about $2,400 annually for a crew of 30.
That said, our experience is specific to a facility with heavy chemical exposure. If your environment is mostly dry and abrasive, the optimal boot will probably be different. I'm not 100% sure what the best option is for a purely construction setting, but a well-known brand with a strong warranty is a safe starting point.
Common Mistakes I've Made (So You Can Avoid Them)
Mistake 1: Only Comparing Unit Price
Everything I'd read about procurement said to negotiate the lowest price per unit. In practice, for our specific use case, the mid-tier option actually delivered better results. Cheap respirators that workers won't wear because they're uncomfortable cost you a lot more in productivity than a quality NIOSH-approved alternative.
Mistake 2: Forgetting to Check Payment Responsibility Per OSHA
I said "we've always bought whatever employees request." They heard "we don't fund PPE requests." We had to backtrack and establish a formal approval process that still allowed employees to request equipment without a blank check. When in doubt, assume you're responsible for paying for PPE—the OSHA standard is employer-funded by default.
Mistake 3: Ignoring the Time Cost of Purchasing
Had 2 hours to decide before a compliance deadline once. Normally I'd get multiple quotes, but there was no time. Went with our usual vendor based on trust alone. It worked out, but I wouldn't recommend it. The right move is to maintain a pre-approved vendor list with standing pricing so you don't have to sacrifice the process when pressure hits.
Final Notes
PPE procurement is about protection, not paperwork. The right process still anchors on one principle: total cost thinking. Price matters, but it's only the beginning. Compliance duties matter. Worker adoption matters. The operational cost of a glove that's 20 cents cheaper but lasts half as long is still a bad deal.
And regarding who pays for PPE: unless you're in one of those narrow exceptions OSHA allows, the answer is the employer. If you're budgeting for 2025, make sure PPE is a line item you control, not a reimbursement queue.
One more thing: I've been buying from makers like Magid for years, not because they're flawless, but because having a direct relationship with the factory helps when we need technical advice—like when we needed cut ratings for a specific knit glove or dielectric properties for rubber boots near live circuits.
Take this with a grain of salt: my data is based on orders from 2020 through early 2025, so pricing will shift. But the process won't. Build the checklist, calculate TCO, document compliance, and you'll do better than most of the industry.
Maeve Callahan
Maeve Callahan is a head-protection analyst covering Type I and Type II hard hats, climbing-style safety helmets, bump caps, chin straps, suspensions, liners, and face-shield carriers. She applies ANSI Z89.1, EN 397, and EN 12492 criteria while comparing impact attenuation, penetration resistance, lateral deformation, electrical class, retention strength, field of vision, mass, fit range, and temperature conditioning. Her guides help EHS teams, contractors, utilities, and buyers select helmet systems for overhead hazards, work at height, electrical exposure, accessory compatibility, and worker acceptance.
Leave a Reply